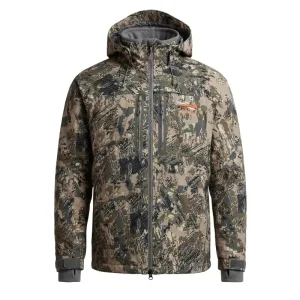
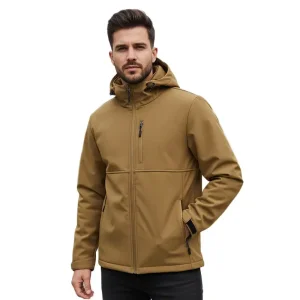
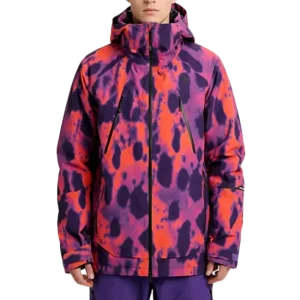
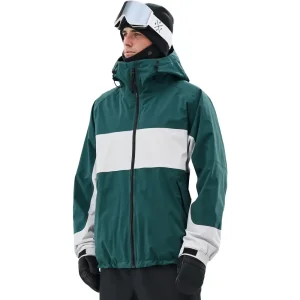
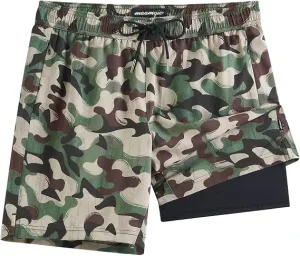
Featured technical garments produced under ISO 9001 and CE certified standards for global enterprise clients.
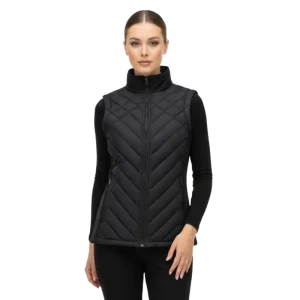
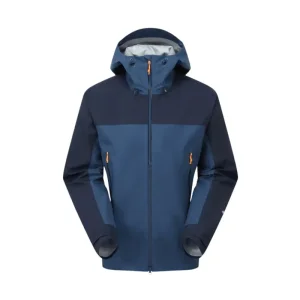
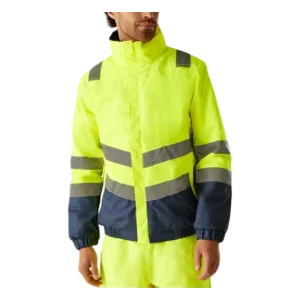
In the global performance outerwear sector, achieving compliance with European Conformity (CE) standards is no longer merely a decorative label—it is a mandatory legal gateway and an engineering benchmark for brand authority. Under European Union Personal Protective Equipment (PPE) Regulation (EU) 2016/425, ski outerwear designed for extreme weather environments, professional alpine work, or high-speed snow sports falls under strict technical surveillance categories.
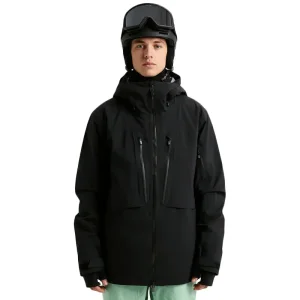
For global sourcing directors and outdoor apparel brand managers, partnering with qualified CE certification ski outerwear factories and manufacturers ensures that garments survive rigorous mechanical, hydrostatic, and thermal testing protocols before reaching retail channels.
Measures waterproofness (hydrostatic pressure resistance) and water vapor resistance (breathability, RET index). Class 4:4 represents the highest performance threshold requiring hydrostatic head ratings exceeding 20,000 mm H₂O post-flexing and post-wash testing.
Evaluates resultant effective thermal insulation ($I_{cler}$) and air permeability ($AP$). Garments undergo thermal mannequin testing down to -30°C, verifying insulation stability under wind velocity exposure.
Strategic placement of passive RECCO® radar reflectors inside garment seam structure. Ensures compliance with avalanche safety norms while preserving 100% seam sealing integrity.
Information Gain Note for Procurement Teams: True CE compliance requires batch-level traceability for every component—from hydrophobic face fabrics and microporous TPU/ePTFE membranes down to flame-retardant threads and waterproof YKK AquaGuard® zippers.
The alpine apparel industry is undergoing a paradigm shift driven by environmental mandates, smart textile integration, and advanced polymer engineering. As a leading technical garment manufacturer, Guangdong Ruiniu Garment Manufacturing Co., Ltd. actively invests in the next generation of outdoor performance technologies.
With international regulations phasing out PFAS and PFC chemistry, our R&D roadmap prioritizes bio-based Polyurethane (PU) and expanded Polyethylene (ePE) membranes. These sustainable 3-layer laminates deliver 20,000mm waterproofing and 15,000 g/m²/24h breathability without halogenated chemicals, retaining water repellency even after 30 industrial wash cycles.
Future ski outerwear integrates zoned thermal insulation. Utilizing 3D thermal imaging technology, synthetic insulation (recycled PrimaLoft® or RDS-certified down) is strategically varied across garment body zones—heavy density on core chest areas (120g/m²), lighter density under arms (60g/m²), and high-stretch laser-vented softshell panels along back heat zones.
To align with global circular economy goals, our design team is engineering 100% Mono-Polyester Ski Outerwear. By matching PET face fabrics, PET hydrophobic membranes, PET seam sealing tapes, and PET insulation fill, the finished jacket can be mechanically recycled at end-of-life without labor-intensive trim separation.
Replacing traditional needle stitching with ultrasonic cutting-welding machinery eliminates stitch-per-inch needle holes entirely. Combined with 13mm micro-tape seam sealing, garment weight is reduced by 15% while stormproof reliability and tensile strength across main stress seams are elevated by 25%.
Global outdoor brands, distributors, and private label importers face unprecedented macro challenges: severe seasonal demand swings, volatile raw material prices, extended freight lead times, and stringent environmental audits. A pure contract sewing plant is no longer sufficient—brands require a strategic supply chain solution provider.
We manage dual-season production planning, balancing winter ski wear and heavy down parkas during peak Q1-Q3 windows with summer technical swim shorts and softshell jackets during off-peak periods, preserving skilled labor continuity year-round.
While industry standard factories demand 1,000+ pieces per style, Ruiniu supports dynamic market testing with lower 100 pcs MOQ per style, enabling brands to seed new technical ski apparel lines with reduced inventory risk.
Accelerating sample development cycles from weeks to days. Our digital pattern-making team utilizes 3D CLO software to simulate fabric drape, stretch elasticity, and thermal fit blocks prior to cutting physical fabric, slashing proto sample lead time to 7–10 days.
Exporting ski outerwear across North America, the European Union, the United Kingdom, and APAC markets demands strict compliance with fragmented chemical safety, environmental protection, and labor regulations.
| Target Region | Mandatory / Voluntarily Certifications | Chemical & Eco Standard | Ruiniu Verification Protocol |
|---|---|---|---|
| European Union (EU) | CE Marking (PPE EU 2016/425), EN 343, EN 342 | REACH SVHC, OEKO-TEX Standard 100 | Full laboratory testing via SGS / Intertek with accredited certificate issuance. |
| North America (US/CA) | ASTM F2732 (Thermal Rating), CPSIA Compliance | PFAS-Free State Regulations (CA AB 1817) | Batch-level chemical screening for fluorine content; Lead & Phthalates testing. |
| Global / Multi-Market | Global Recycled Standard (GRS), RDS Down | bluesign® Approved Fabric Sourcing | Chain-of-custody Transaction Certificates (TC) provided per shipment PO. |
Guangdong Ruiniu Garment Manufacturing Co., Ltd. provides full localization documentation support, including dual-language care label compliance (translated into 15+ languages), tariff classification HS code guidance (e.g., 6201.93 / 6202.93 for synthetic ski wear), and country-of-origin certification.
Located in Nanhai District, Foshan City, Guangdong Province, Guangdong Ruiniu Garment Manufacturing Co., Ltd. (founded in 2002) stands at the epicenter of China’s most advanced apparel manufacturing ecosystem. Spanning over two decades of dedicated outdoor apparel production, our facility merges traditional textile craftsmanship with Industry 4.0 smart manufacturing automation.
Utilizing automated Gerber spreading and CNC laser cutting tables, fabric nesting markers consistently exceed 88% efficiency. This minimizes waste on expensive 3-layer waterproof membranes and lowers raw material landed costs directly for our clients.
Our dedicated sample development room is staffed by 12 master technicians capable of translating hand sketches, competitor samples, or raw tech packs into production-ready CAD patterns within 48 hours.
To guarantee zero defect delivery, every production batch passes through our rigorous 3-tier QC mechanism aligned with AQL 2.5 (or AQL 1.0 upon request):
Use this specification benchmark when constructing your technical outerwear tech pack or requesting an OEM quotation from our engineering team.
| Garment Tier | Outer Face Shell | Membrane / Lamination | Seam Sealing & Hardware | CE & Technical Performance Target |
|---|---|---|---|---|
| Pro Expedition 3L Hard Shell | 100D Nylon 6.6 Ripstop (180 g/m²) | Microporous ePTFE / PU 3-Layer Bonded | 13mm Micro-Tape; YKK AquaGuard® Vislon Zips | Hydrostatic: 20,000mm+ | RET < 6 | RECCO® Equipped | EN 343 Class 4:4 |
| Resort Performance 2.5L Insulated | 75D Recycled Polyester Plain (130 g/m²) | Hydrophilic TPU 2.5L Print Membrane | 20mm PU Seam Tape; Pit Zips with Mesh Guard | Hydrostatic: 15,000mm | MVTR: 10,000 g/m²/24h | 100g PrimaLoft® Fill | EN 342 |
| Freeride Softshell Jacket | 75D 4-Way Stretch Polyester + Spandex | 3-Layer Bonded Fleece Backer (300 g/m²) | Reinforced Bar-tacking; Laser-cut Hem Cuffs | Hydrostatic: 8,000mm | Windproof < 5 CFM | DWR PFC-Free finish |
| Alpine Down Parka | 20D Micro-Ripstop Nylon (Down-Proof) | 2-Layer Laminated Windproof Coating | Baffle Box Construction; Double Storm Flap | 800 Fill Power RDS Goose Down (90/10) | Warmth rated to -30°C | EN 342 Certified |
Direct technical answers regarding order processing, CE certification verification, compliance testing, and production lead times.
Explore our complete OEM/ODM production categories built for international performance brands.