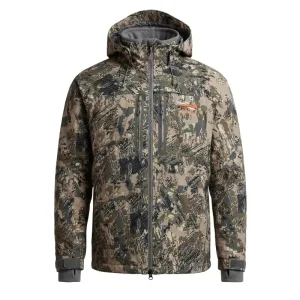
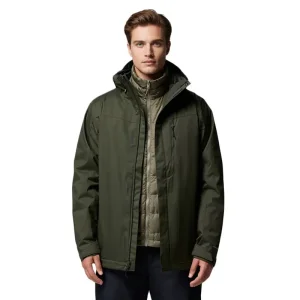
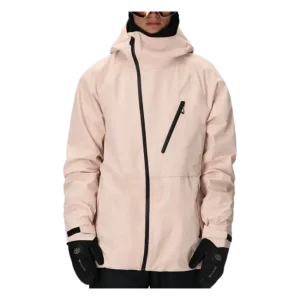
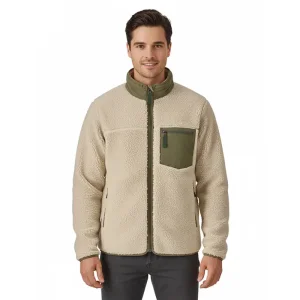
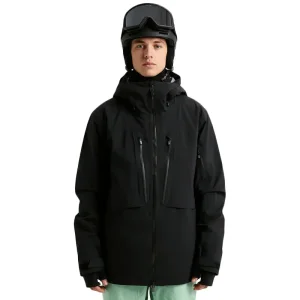
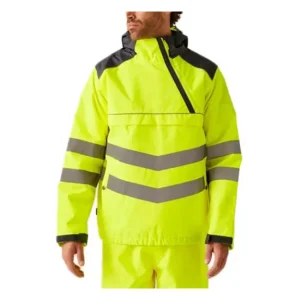
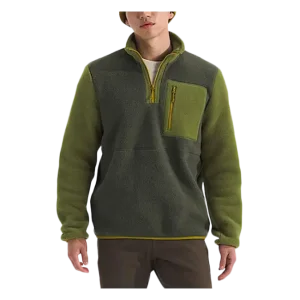
Explore our factory-engineered waterproof jackets, technical skiwear, and insulated garments developed for global brands and commercial enterprises.
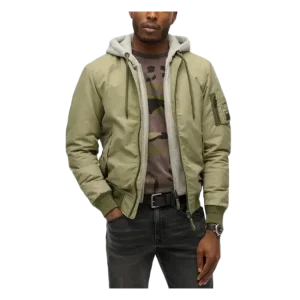
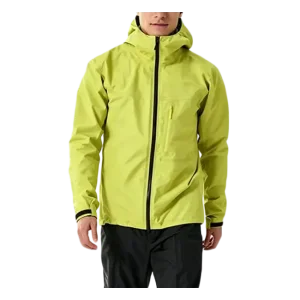
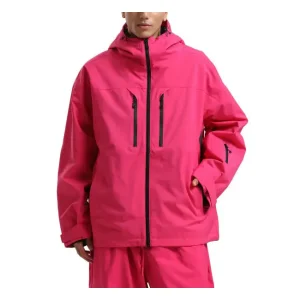
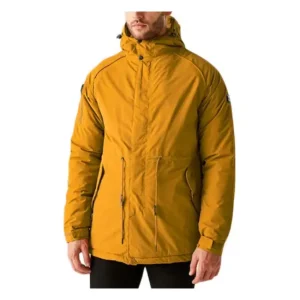
Navigating modern technical outerwear sourcing requires balancing membrane performance, cost structures, low MOQs, and stringent environmental compliance across global retail markets.
In today's competitive commercial apparel landscape, institutional procurement leads, brand owners, and safety distributors require far more than basic cut-and-sew garment operations. Sourcing a custom waterproof outdoor jacket involves managing complex multi-layer material laminations, certified seam-sealing techniques, and strict quality control standards.
Buyers face increasing supply chain headwinds, including volatile lead times, fluctuating raw fabric minimums, and strict ESG requirements enforced by European and North American customs authorities. Modern outdoor brands demand direct mill relationships, transparent bill-of-materials (BOM), and factory partners capable of maintaining structural integrity across extreme sub-zero alpine and industrial work environments.
A single failure in seam lamination or membrane degradation can result in costly consumer returns, brand equity loss, and warranty liabilities. Reliable manufacturing services employ a multi-stage Quality Assurance framework:
Understanding 2-Layer, 2.5-Layer, and 3-Layer hardshell lamination technology for specialized industrial and commercial outerwear applications.
| Laminate Type | Construction Layering | Hydrostatic Head (ISO 811) | Breathability (MVTR JIS L1099) | Target End-Use Application |
|---|---|---|---|---|
| 2-Layer (2L) | Outer Face Fabric + Laminated Membrane (Hanging Mesh Liner) | 10,000 mm – 15,000 mm | 8,000 g/m²/24h | Urban Lifestyle, Resort Skiing, Light Workwear |
| 2.5-Layer (2.5L) | Face Fabric + Membrane + Raised Protective Internal Print | 10,000 mm – 20,000 mm | 12,000 g/m²/24h | Packable Rain Shells, Fast-Trekking, Running Jackets |
| 3-Layer (3L) | Face Fabric + Microporous PTFE/TPU Membrane + Tricot Backer | 20,000 mm – 30,000 mm | 15,000 – 25,000 g/m²/24h | Extreme Mountaineering, Expedition Ski Wear, Offshore Tactical |
| Bonded Softshell | Woven Stretch Face + Breathable Film + Microfleece Fleece Backer | 8,000 mm – 10,000 mm | 5,000 – 8,000 g/m²/24h | Cold Weather Active Outerwear, Utility Work Uniforms |
Our factories utilize expanded PTFE (ePTFE), Thermoplastic Polyurethane (TPU), and Bio-based Polyurethane membranes. Microporous membranes contain billions of microscopic pores per square inch—each pore 20,000 times smaller than a water droplet, yet 700 times larger than a water vapor molecule, guaranteeing complete waterproof protection with high breathability.
In compliance with global environmental mandates (EU REACH & US State PFAS bans), our manufacturing lines transition seamlessly to C0 PFC-Free Durable Water Repellent (DWR) treatments. Utilizing advanced silicon and plant-based chemistries, our face fabrics achieve initial 100-point spray ratings (ISO 4920) while retaining 80 points after 20 continuous industrial wash cycles.
Sewing needles puncture face fabrics, creating thousands of micro-holes. Our high-speed pneumatic hot-air seam-sealing machinery applies 3-layer PU and micro-tapes (ranging from 13mm to 22mm widths) over all needle stitch lines. Dual heating zones ensure full melt-adhesion without scorching delicate face fabrics or degrading thermal insulation.
Analyzing the global shift in technical outerwear production: Foshan and Guangdong supply chain clusters vs. Southeast Asia assembly lines.
While basic cotton apparel assembly has shifted to lower-cost regions in Southeast Asia, high-complexity outerwear—specifically custom 3L waterproof hardshells, RECCO® equipped ski jackets, and down-filled parkas—remains heavily anchored in Guangdong, China.
The proximity to specialized weaving mills, membrane lamination plants, waterproof zipper manufacturers (YKK, SBS), and precision mold makers enables rapid prototype iterations (7–10 days) and shorter production preparation cycles. Our Foshan factory combines skilled technical labor with automated CAD pattern nesting and laser cutting tables to optimize fabric yield over 88%.
Modern waterproof jacket factories require significant capital expenditure in automated equipment to guarantee repeatable technical performance:
Delivering fully certified waterproof garments aligned with European Union, North American, and Australian retail and safety workwear directives.
Every fabric roll processed in our facility undergoes chemical safety screening. We provide verifiable mill certificates for OEKO-TEX® Standard 100 Class I/II, bluesign® system approval, and Global Recycled Standard (GRS) certification for recycled polyester and nylon face fabrics.
For commercial workwear accounts, our reflective waterproof jackets are engineered to meet EN ISO 20471 Class 2 / Class 3 (High Visibility) and EN 343 Class 4:4 (Rain Protection). Retaining retro-reflective efficiency up to 50 industrial laundry cycles.
All natural insulation sourced for custom down jackets adheres to the Responsible Down Standard (RDS) or Global Traceable Down Standard (TDS). Full supply chain traceability from farm to factory ensures zero live-plucking and zero force-feeding.
Expert answers to critical procurement questions for apparel buyers, OEM/ODM clients, and supply chain directors.
Discover our specialized lines including RECCO® avalanche safety jackets, 3-in-1 modular systems, hi-vis reflective safety workwear, and fleece mid-layers.